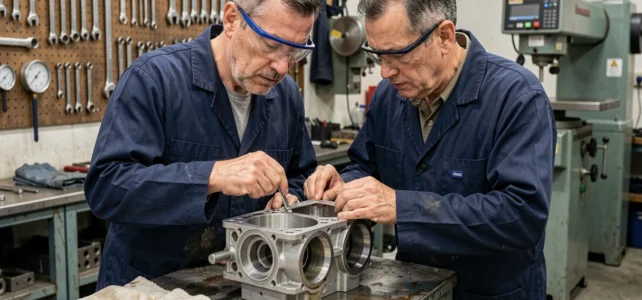
The resurfacing of a cylinder head is not just a simple pass on a machine. Depending on the type of engine, the material of the cylinder head, and the origin of the defect, the accepted tolerances, machining techniques, and risks vary significantly. Comparing these parameters helps to understand why two cylinder heads exhibiting the same symptom, a flatness defect, are not treated in the same way.
Flatness Tolerances and Machining Limits According to Cylinder Head Material
The material of the cylinder head directly determines the margin of maneuver available during resurfacing. Manufacturers set flatness tolerances that vary from one engine to another, but the distinction between cast iron and aluminum remains the primary sorting criterion.
| Criterion | Cast Iron Cylinder Head | Aluminum Cylinder Head |
|---|---|---|
| Sensitivity to thermal deformation | Moderate | High |
| Risk of local overheating during machining | Low | Significant (rapid expansion) |
| Typical flatness tolerance | Variable by manufacturer, often more permissive | Variable by manufacturer, often stricter |
| Minimum residual thickness | Generally wider margin | Narrow margin, to be systematically checked |
| Recommended surface finish | Classic flat grinding machine | CNC finishing machining for uniformity |
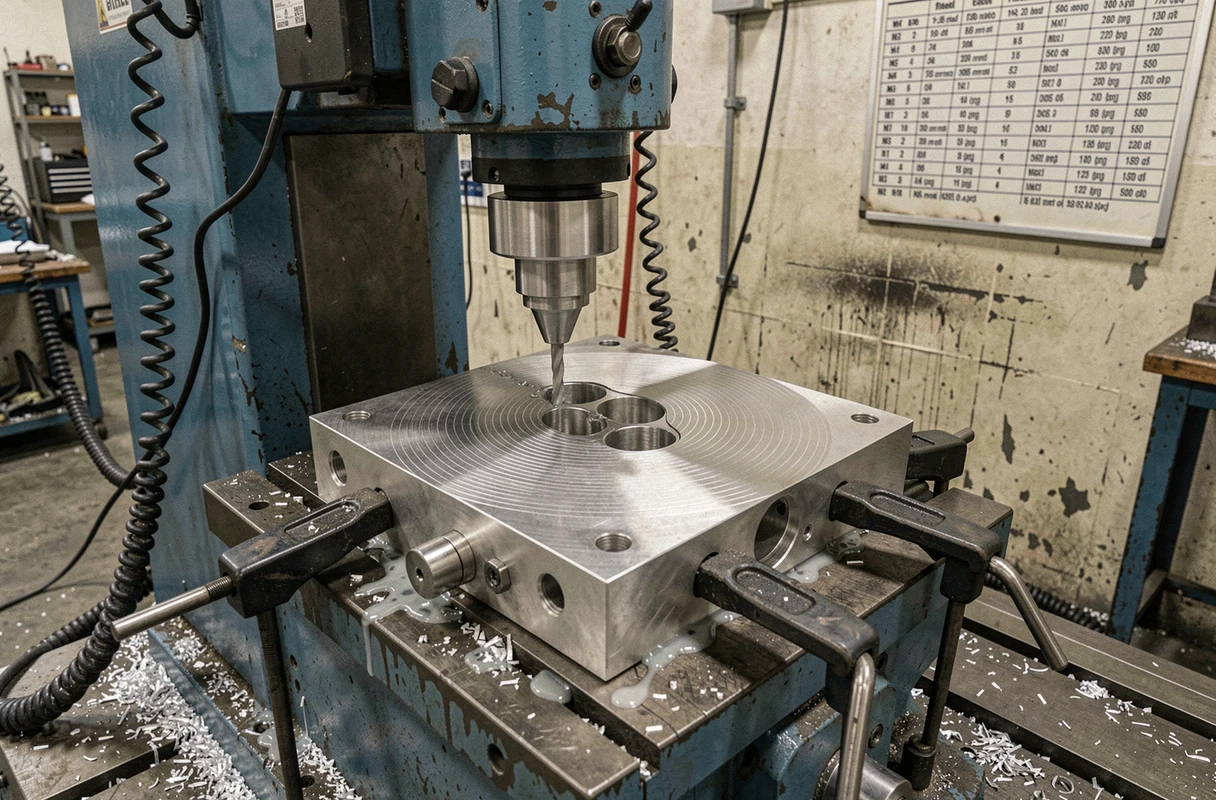
On an aluminum cylinder head, material removal is more constrained. The alloy expands rapidly due to the heat generated by the grinding wheel, which can distort measurements during machining. CNC finishing machining reduces this risk by providing a more uniform and reproducible finish than a manual process.
For a cast iron cylinder head, the classic flat grinding machine remains suitable in most cases. However, any aluminum cylinder head justifies enhanced control of the residual thickness after resurfacing, as going below the manufacturer’s threshold alters the compression ratio and places abnormal stress on the distribution.
A detailed guide on cylinder head resurfacing and machining helps to better understand the critical steps of this intervention.
Flatness Control and Leak Testing: Two Distinct Measures
Many contents confuse flatness control and leak testing. These two operations occur at different times and do not detect the same defects.
Flatness control is performed before any machining. The cylinder head is placed upside down on a flat surface or workbench. A precision rule, placed edgewise across and then diagonally, allows for the identification of light spots. The insertion of a thickness gauge between the rule and the mating surface provides the measurement of the defect.
If the gauge does not pass, the surface is within tolerances. If it passes, the cylinder head requires resurfacing. The measurement must be taken at several points, as a cylinder head can be locally warped without the defect being visible to the eye.
Leak testing is a distinct test, performed by applying hydraulic pressure to the cylinder head. It detects internal cracks in the water or oil circuits, which are invisible on the surface. A flat cylinder head can be cracked, and a cracked cylinder head can appear flat. Not separating these two controls exposes one to machining an irreparable part.
Critical Steps of Cylinder Head Resurfacing in the Workshop
The resurfacing itself is just one link in a chain of operations. Skipping a step or reversing the order compromises the final result.
- Complete disassembly of the cylinder head (valves, springs, guides, gaskets) and thorough cleaning to eliminate deposits of carbon, burnt oil, and corrosion before any measurement
- Flatness control at several points with a precision rule and thickness gauges, followed by leak testing through pressurization
- Verification of the residual thickness of the cylinder head to confirm that the planned material removal will not go below the manufacturer’s threshold
- Resurfacing on a flat grinding machine or CNC machining, with light passes to avoid any local overheating of the alloy
- Post-machining dimensional control (flatness, roughness) and verification of compliance with manufacturer specifications
The initial cleaning is often underestimated. A residue of carbon of just a few tenths of a millimeter is enough to distort the flatness measurement and cause excessive material removal.
Reassembly and Torque: What Determines the Gasket’s Integrity
A perfect resurfacing is useless if the reassembly is done poorly. The torque of the cylinder head bolts and the tightening order are the two parameters that determine the distribution of pressure on the gasket.
Each manufacturer imposes a specific tightening pattern, generally spiraling from the center to the outside, and a progressive torque in several passes. Not respecting this order creates areas of uneven stress that deform the freshly machined cylinder head.
- Use a calibrated torque wrench, never a hand wrench “by feel”
- Respect the supplementary tightening angle when the manufacturer prescribes it (angular tightening after the initial torque)
- Systematically replace single-use cylinder head bolts (elastic limit bolts), as their reuse distorts the actual torque applied
Reused bolts can yield or lose their tension without any external signs, leading to a gradual loss of sealing of the cylinder head gasket.
Engine Break-in After Cylinder Head Resurfacing
The break-in after reassembly is rarely addressed in mainstream content. After resurfacing, limiting heavy loads and high RPMs during the first kilometers allows the machined surfaces, the new gasket, and the valve seats to gradually adapt.
Driving immediately at full load after reassembling a resurfaced cylinder head stresses the new gasket before it has reached its optimal compression. The risk is an early loss of sealing, precisely the defect that the intervention aimed to correct.
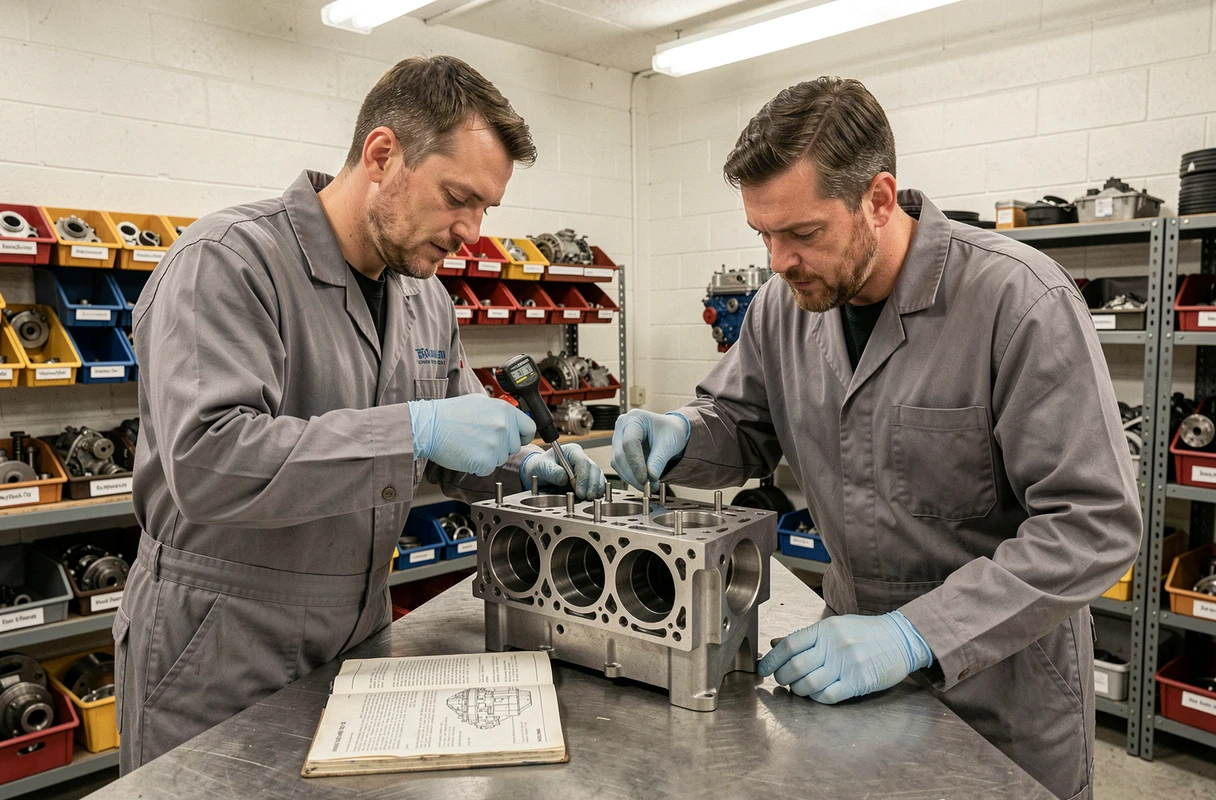
The reliability of a cylinder head resurfacing depends as much on the preliminary checks and reassembly as on the machining itself. A sloppy flatness measurement, an omitted leak test, or approximate tightening negates the benefits of a resurfacing performed correctly.